Our 3-Stage
Manufacturing Process
Under one 1.5 lac sq ft roof in Ludhiana, raw yarn transforms into high-grade knitted fabric through precision circular knitting, computerized softflow dyeing, and advanced compacting finishing.
1.5 Lac
Sq Ft Plant
15,000 Kg
Daily Capacity
< 0.8
Delta E Match
100%
In-House ETP
From Raw Yarn to Finished Fabric
Click into each core stage to explore its specialized machinery, engineering parameters, and quality control protocols.
Knitting & Manufacturing
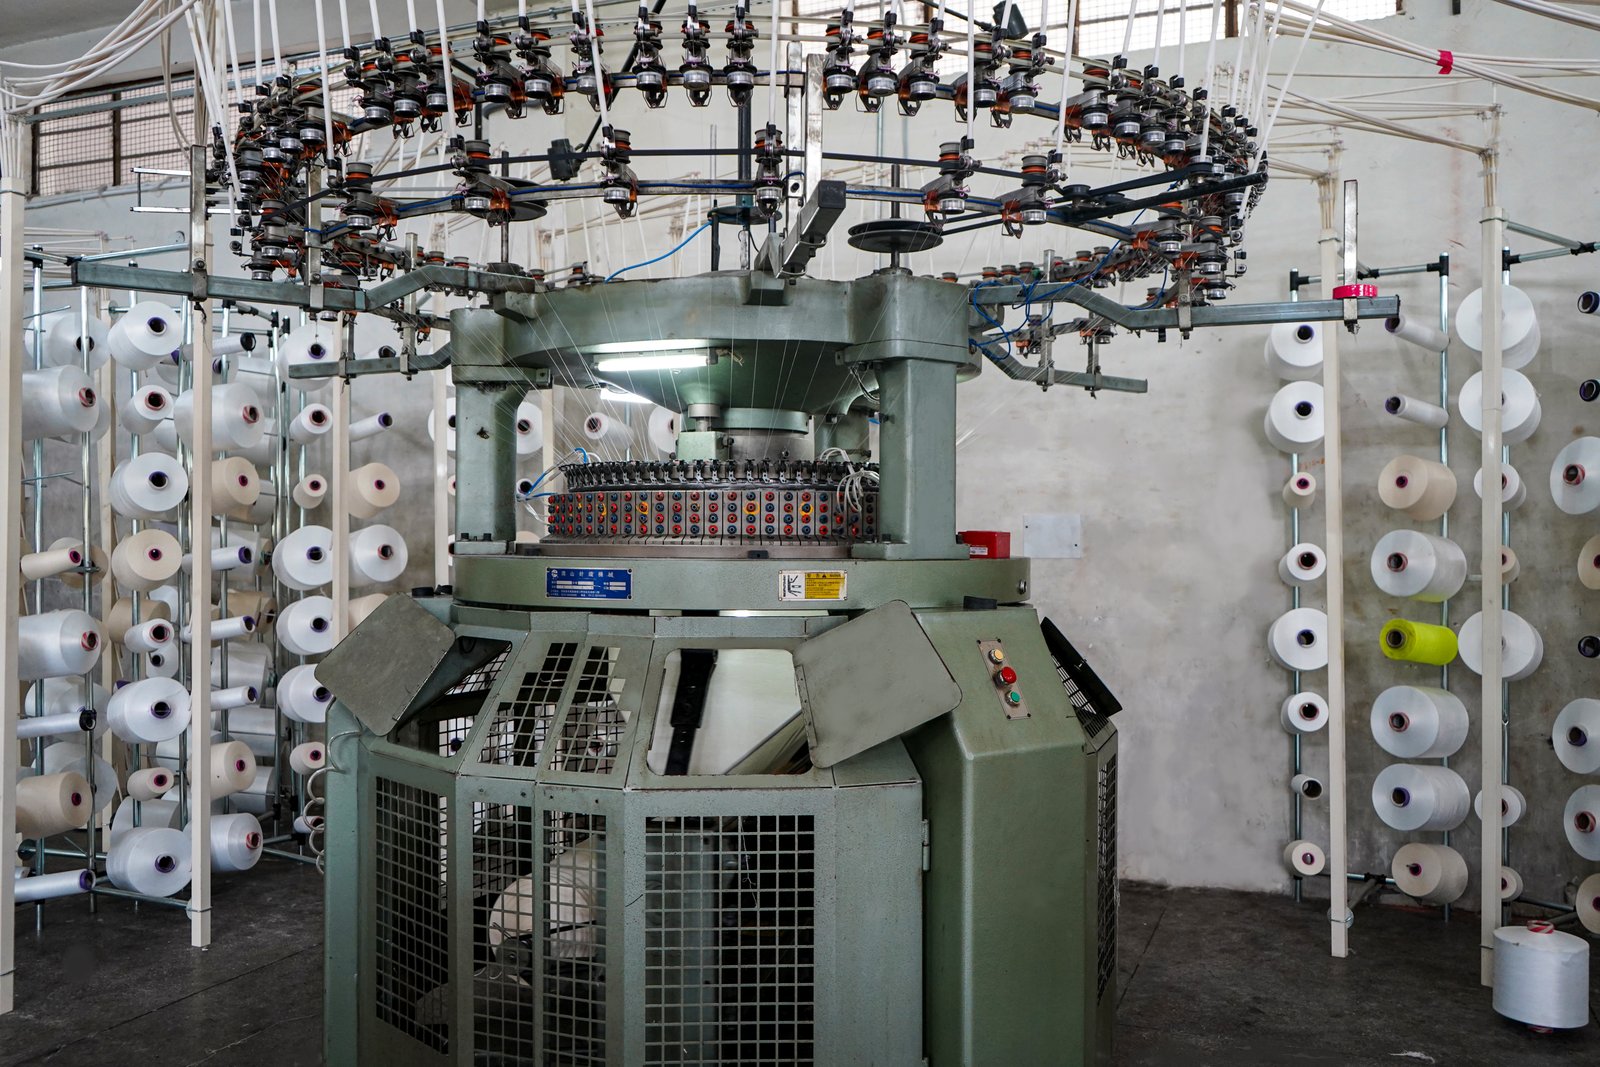
Circular Knitting Machinery & Greige Fabric Formation
Raw combed, carded, and spun yarns are transformed into precision knitted greige fabrics using high-gauge multitrack circular knitting machines. Every stitch loop is engineered for exact GSM, course-wale density, and elastic recovery.
15,000+ Kg
Daily Output
20G – 34G
Gauge Range
99.8%
Loop Uniformity
Dyeing & Color Chemistry
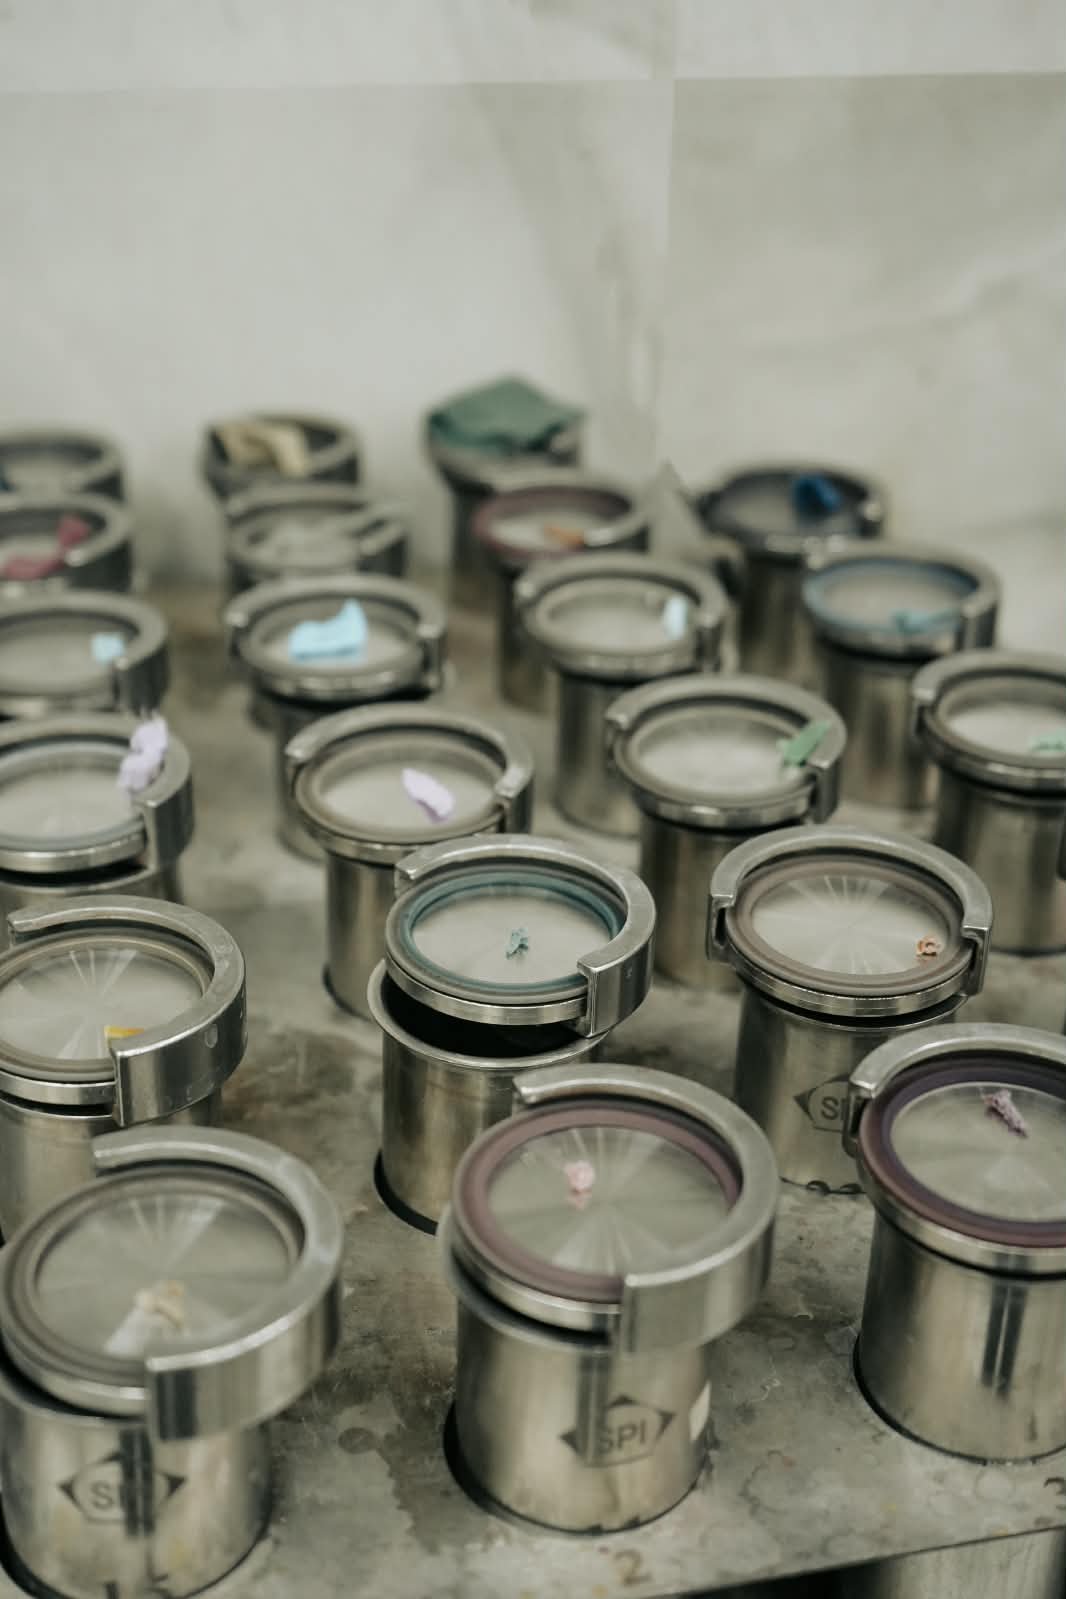
Softflow Dyeing Vessels & Computerized Color Kitchen
Greige fabrics undergo enzymatic bio-polishing, scouring, and automated softflow dyeing in low-liquor ratio vessels. Using spectrophotometer recipe formulations, we achieve precise shade consistency with Delta E under 0.8 across repeat dye lots.
< 0.8
Delta E Tolerance
50–1200 Kg
Batch Capacity
Grade 4.5+
Fastness Rating
Advanced Fabric Finishing
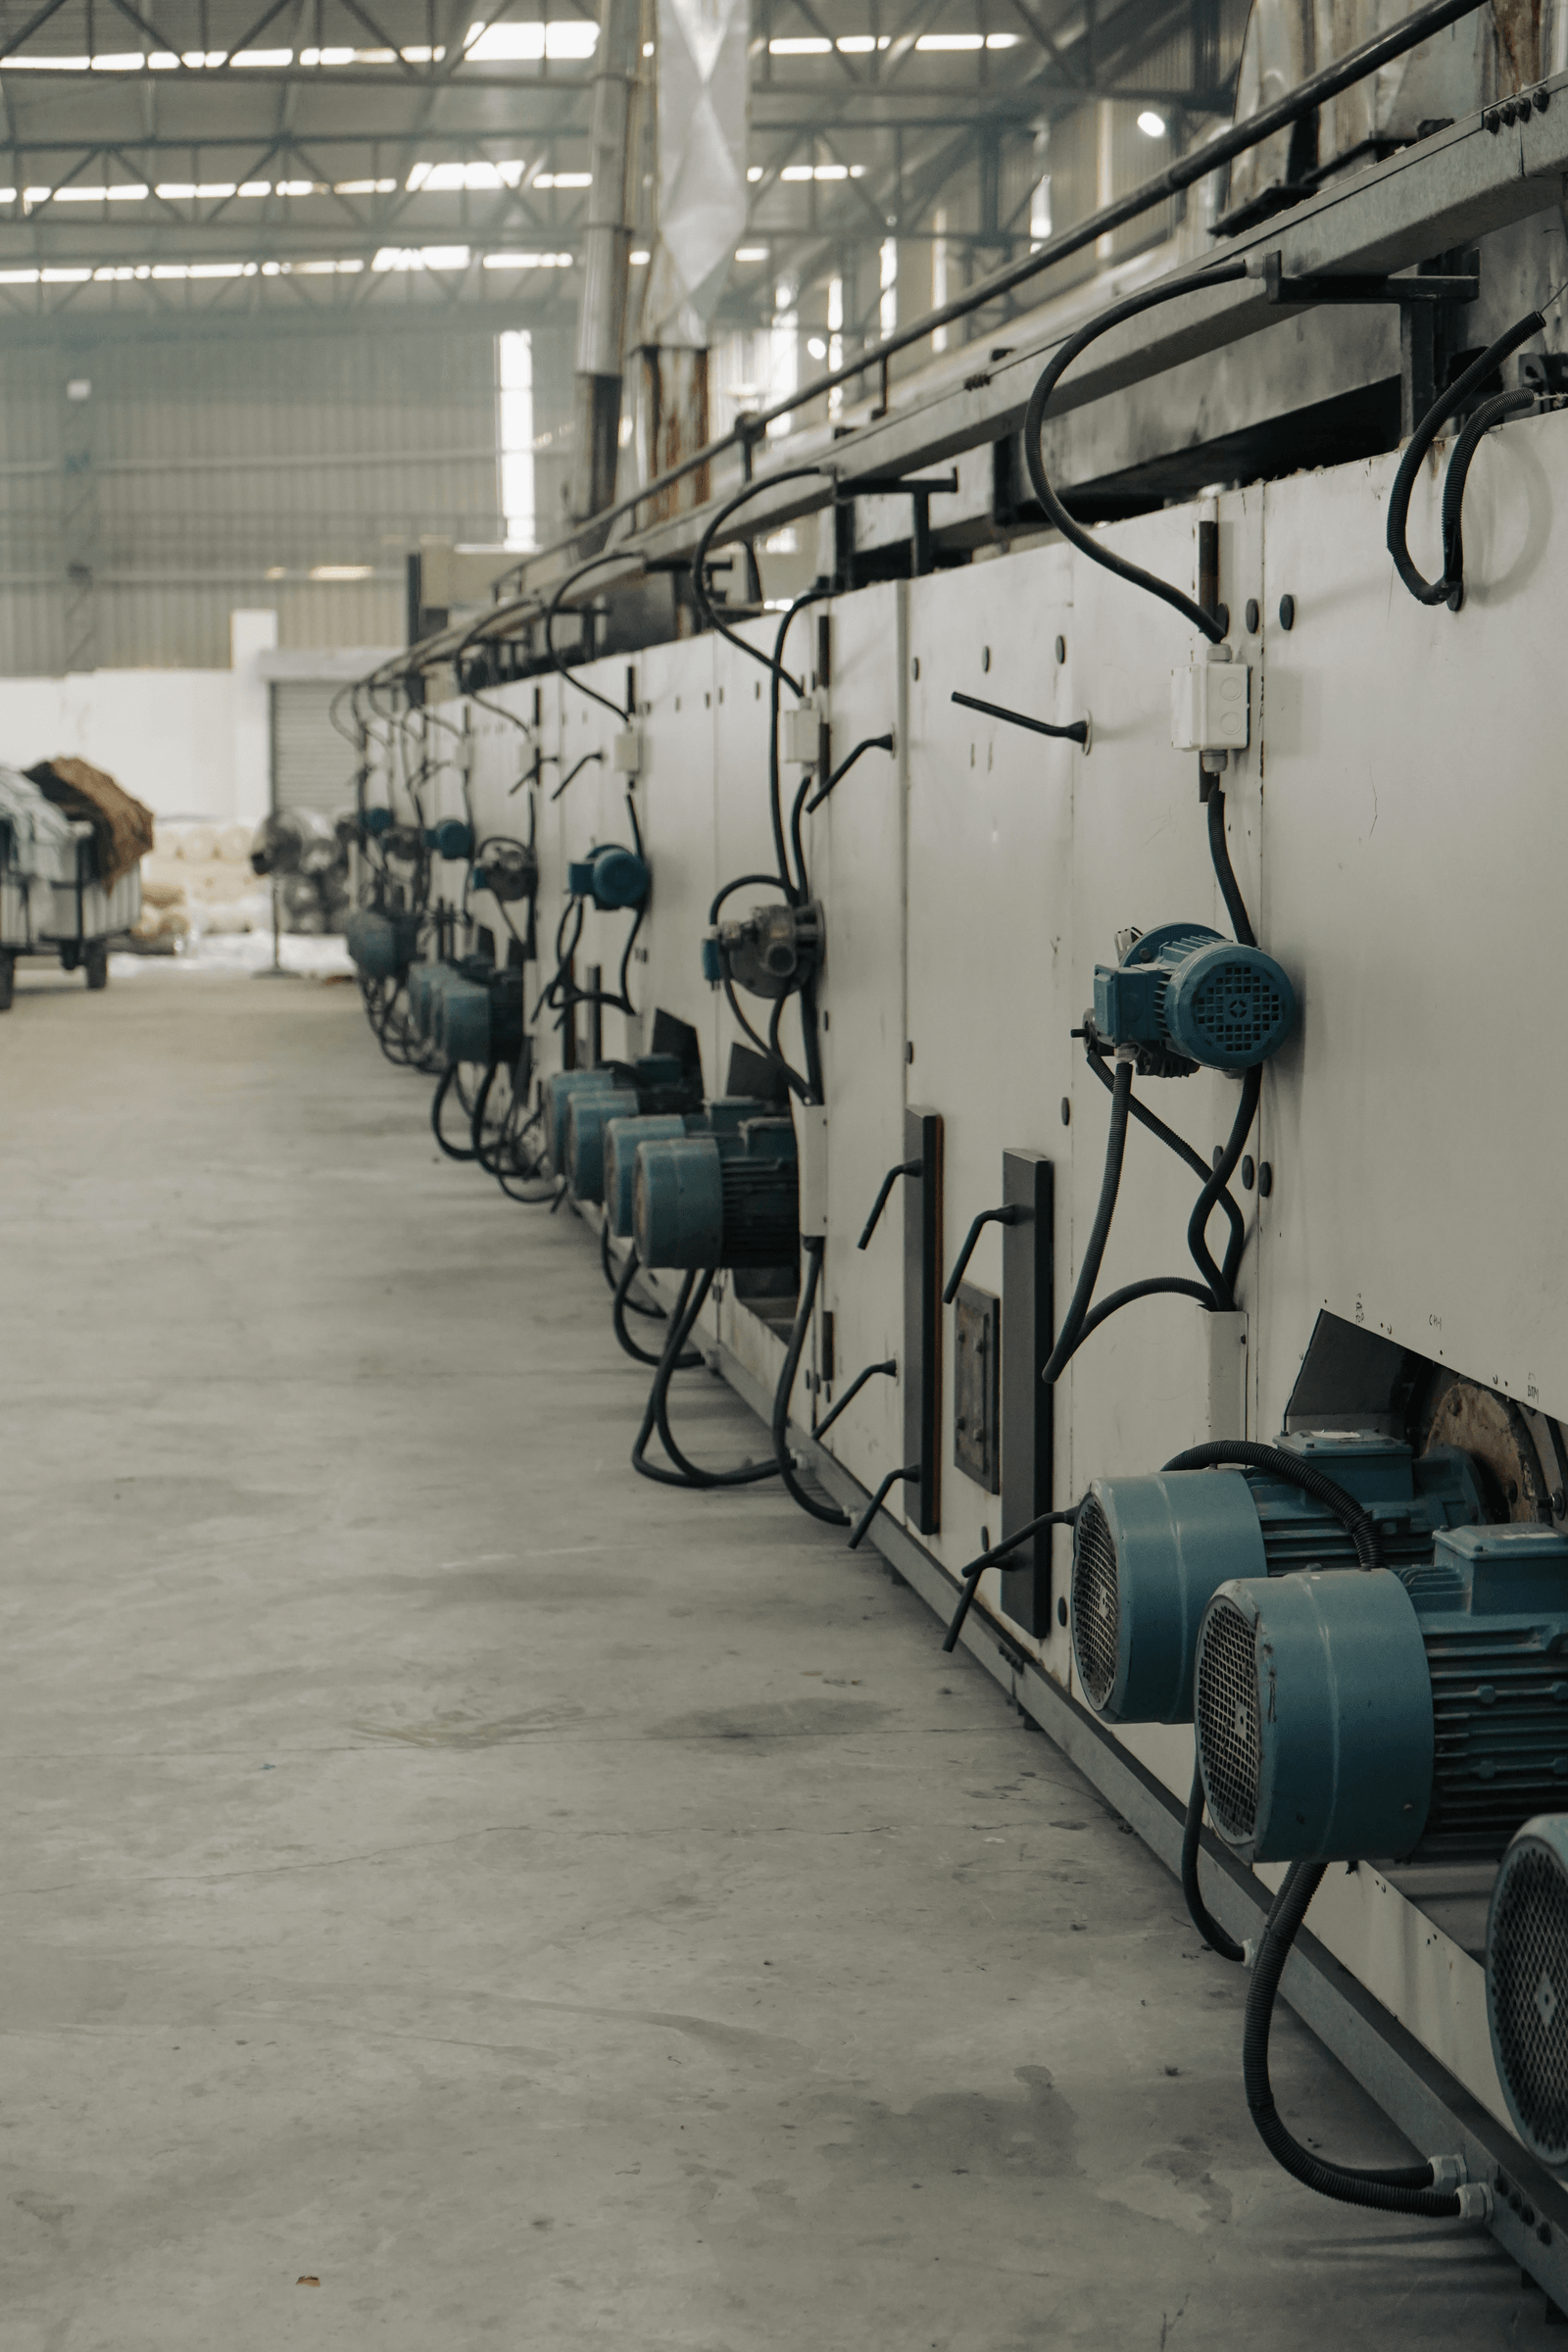
Stenter Frames, Felt Compactor & 4-Point Grading
Dyed fabrics pass through multi-chamber stenter frames, felt calender compactors, and heavy-duty raising units. We lock in dimensional stability, eliminate spirality, control residual shrinkage under 3%, and produce luxurious handfeels.
< 3.0%
Residual Shrinkage
< 2.0%
Spirality Control
3 Tiers
Inspection Stages
Every Metre Tested for Exact Tolerance
Our quality assurance is built into every step. From raw yarn arrival to circular knitting, softflow dye chemistry, compacting, and final dispatch — our in-house lab tests every batch for GSM consistency, shrinkage under 3%, and wash fastness.